What is Soybean White Flake? Why It’s Critical for High-Quality Protein Processing
for protein processing
- ✓ Soybean white flake production requires low-temperature desolventizing technology to maintain protein solubility above 90%
- ✓ Food-grade soybean white flake commands a premium price 25–35% higher
Introduction
According to the USDA 2024 Oilseeds: World Markets and Trade report, global soybean production reached 384 million metric tons in 2024, with 85% utilized for protein processing. This data highlights the central position of the soybean protein industry in the global food supply chain and the plant-based protein market.
In the protein processing value chain, soybean white flake serves as a critical intermediate product connecting oilseed pressing with deep protein processing. Its quality directly impacts the functional properties and market value of the final protein products. However, many factories face quality bottlenecks in traditional processing, including protein denaturation, decreased solubility, and excessive solvent residue, which prevents them from increasing product value.
This article will provide an in-depth analysis of the technical definition, production process, quality standards, and equipment selection for soybean white flake, helping plant owners and project decision-makers understand how to enhance product competitiveness through low-temperature process optimization and enter the high-value-added food-grade protein market.
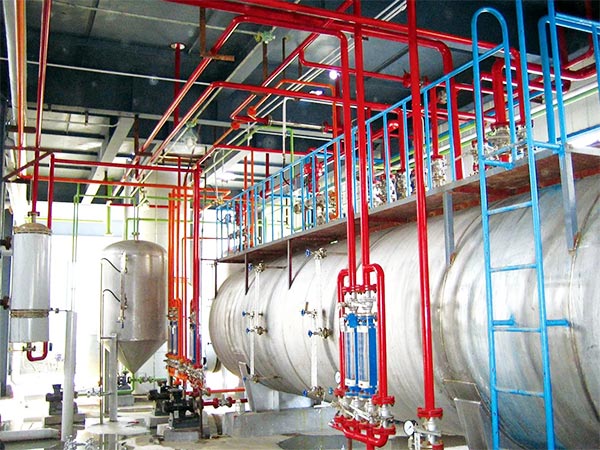
Understanding Soybean White Flake – Definition and Core Value
What Makes White Flake Different from Regular Soybean Meal?
The key difference between soybean white flake and regular soybean meal lies in the control of processing temperature. According to the Soy Protein Council 2024 Soy Protein Processing Guidelines, regular soybean meal is typically desolventized at temperatures of 105-110°C, while white flake is strictly controlled within the 60-80°C range. This temperature difference results in significant distinctions in the functional properties of the two products:
| Quality Parameter | Regular Soybean Meal | White Flake | Improvement |
|---|---|---|---|
| Protein Solubility (NSI) | 45-55% | 80-90% | +70-100% |
| Protein Denaturation Rate | 25-35% | 5-8% | -75-80% |
| Solvent Residue | 800-1200 ppm | <500 ppm | -50-60% |
| Color (Hunter Lab) | L-value 55-60 | L-value 70-75 | +25-35% |
Protein solubility is a key indicator for evaluating white flake quality, directly affecting the efficiency of subsequent protein extraction processes. According to the Food and Agriculture Organization (FAO) 2023 Plant Protein Quality Assessment standard, high-quality white flake should maintain protein solubility above 85%.
Economic Value in Protein Supply Chain
According to the Grand View Research 2024 Plant-Based Protein Market report, the global plant-based protein market reached $14.2 billion and is projected to grow at a CAGR of 9.4% to $25.8 billion by 2030. In this value chain, food-grade white flake serves as a critical upstream raw material with significant market premiums:
- Feed-grade soybean meal: $380-420/ton
- Food-grade white flake: $520-580/ton
- Value premium: +25-35%
This premium is not merely a price difference but reflects the superior functional properties that food-grade white flake delivers to downstream applications. For producers, the ability to consistently produce white flake meeting international standards means access to premium markets and higher profit margins.
Production Process – How CHEMSTA’s Low-Temperature Technology Ensures Quality
Critical Process Control Points
The production of high-quality soybean white flake requires precise control at multiple stages:
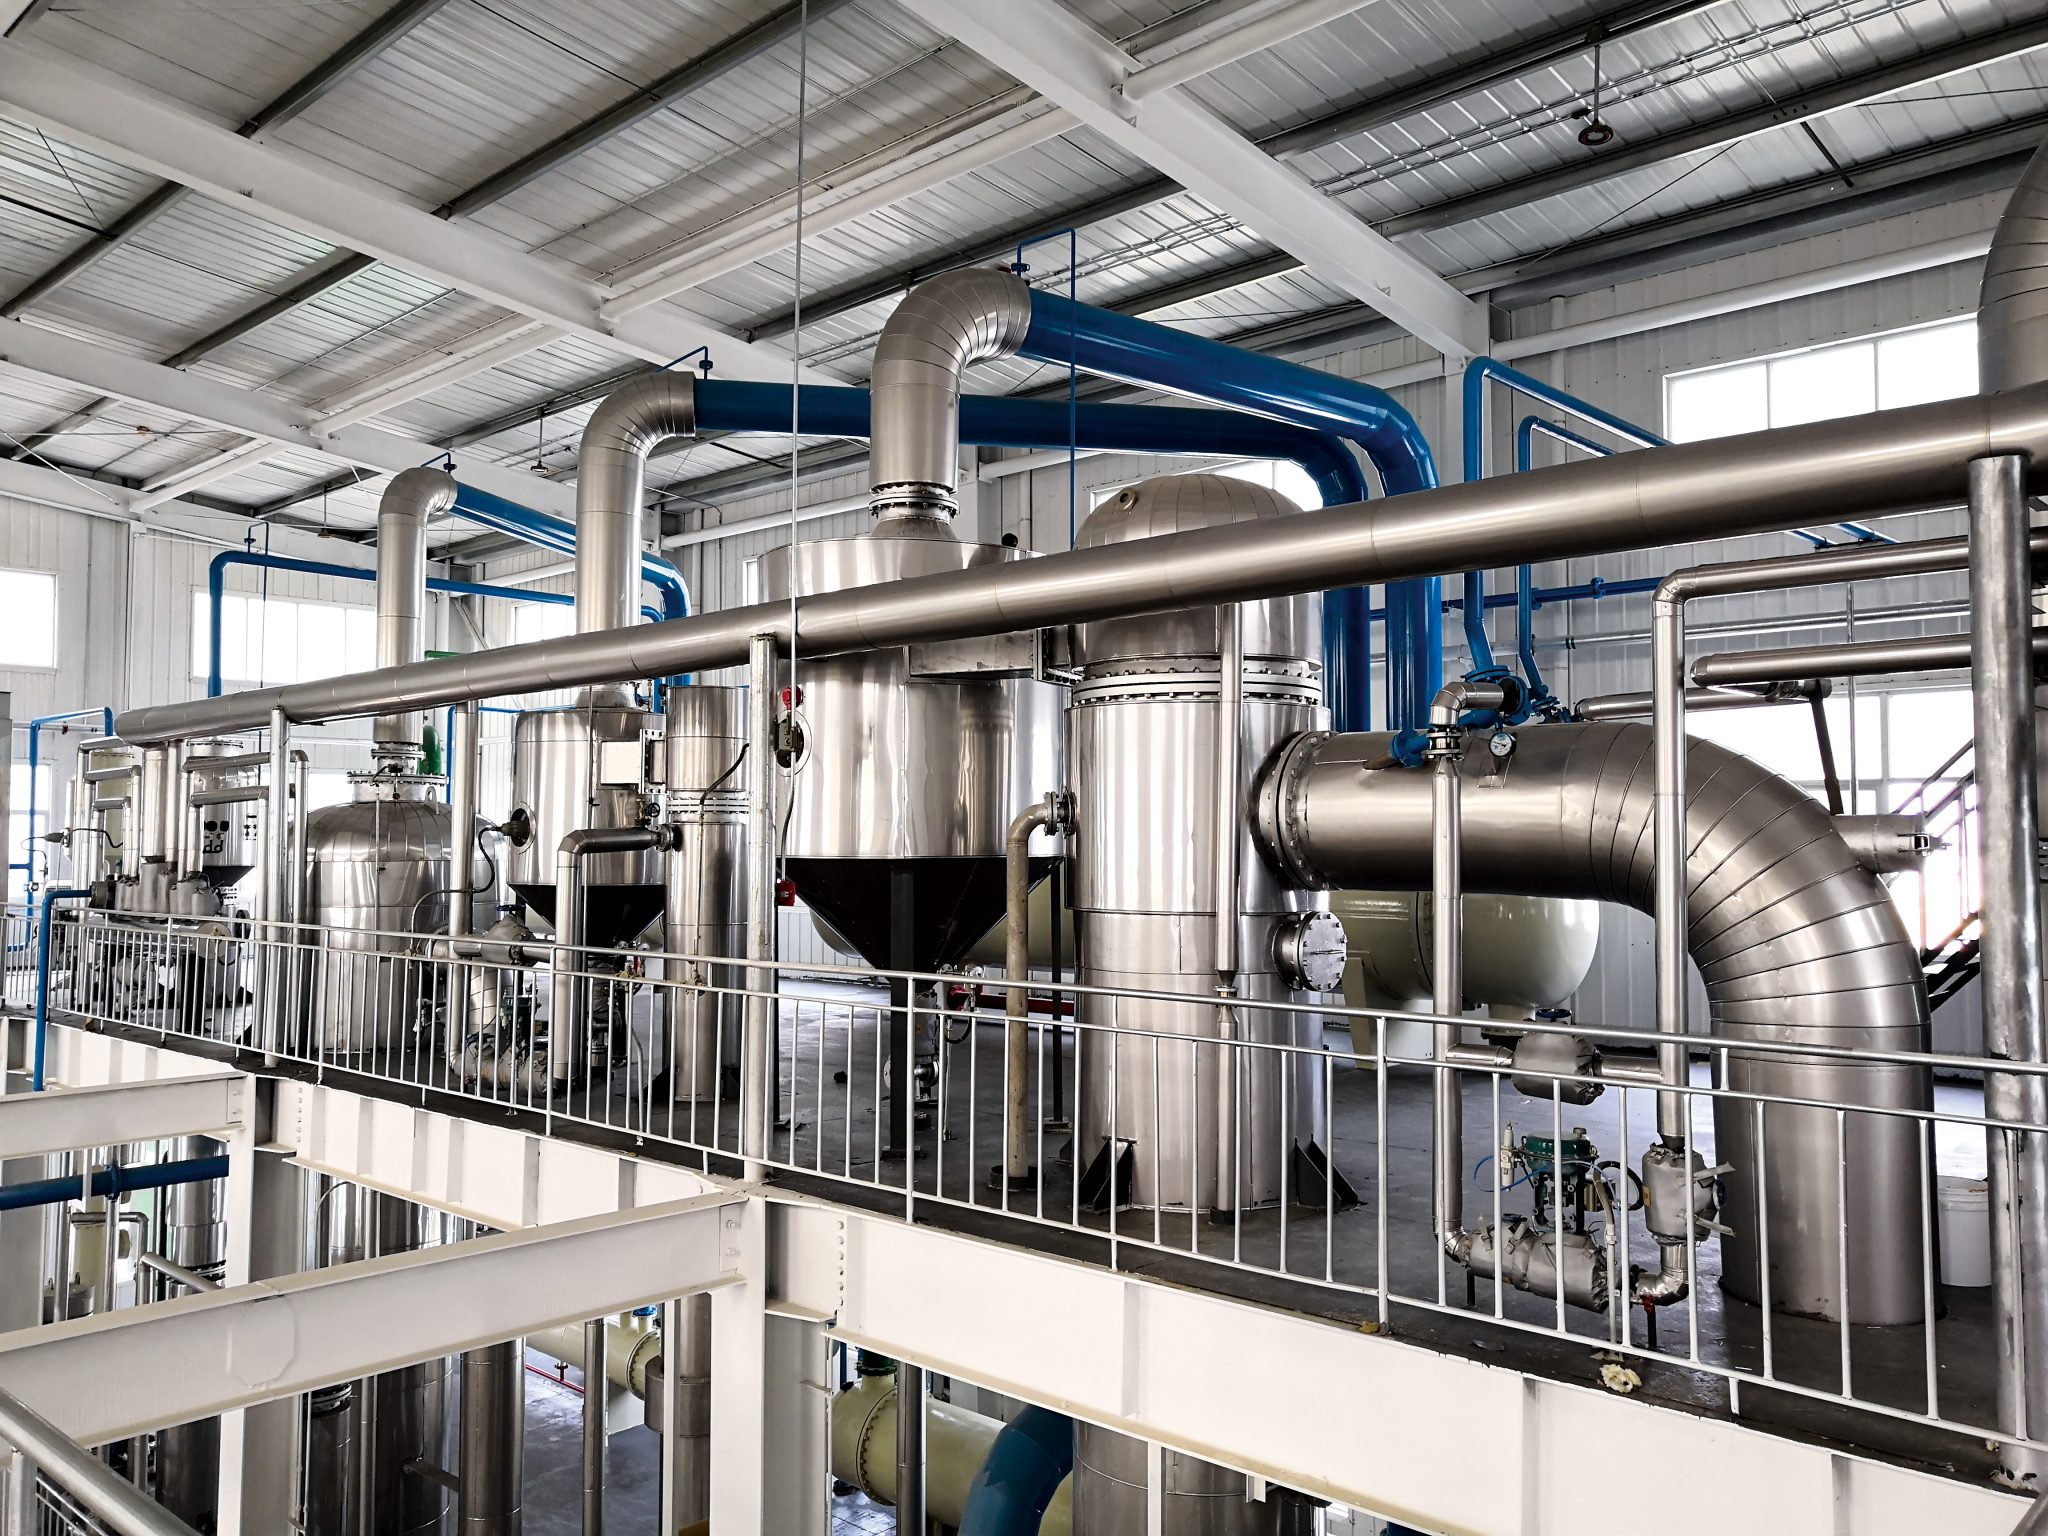
- Solvent Extraction Stage: Utilizing a drag chain extractor for counter-current extraction at 50-55°C with an extraction time controlled at 30-40 minutes. This ensures oil extraction rates reach 98.5% and above while minimizing solvent exposure time for proteins.
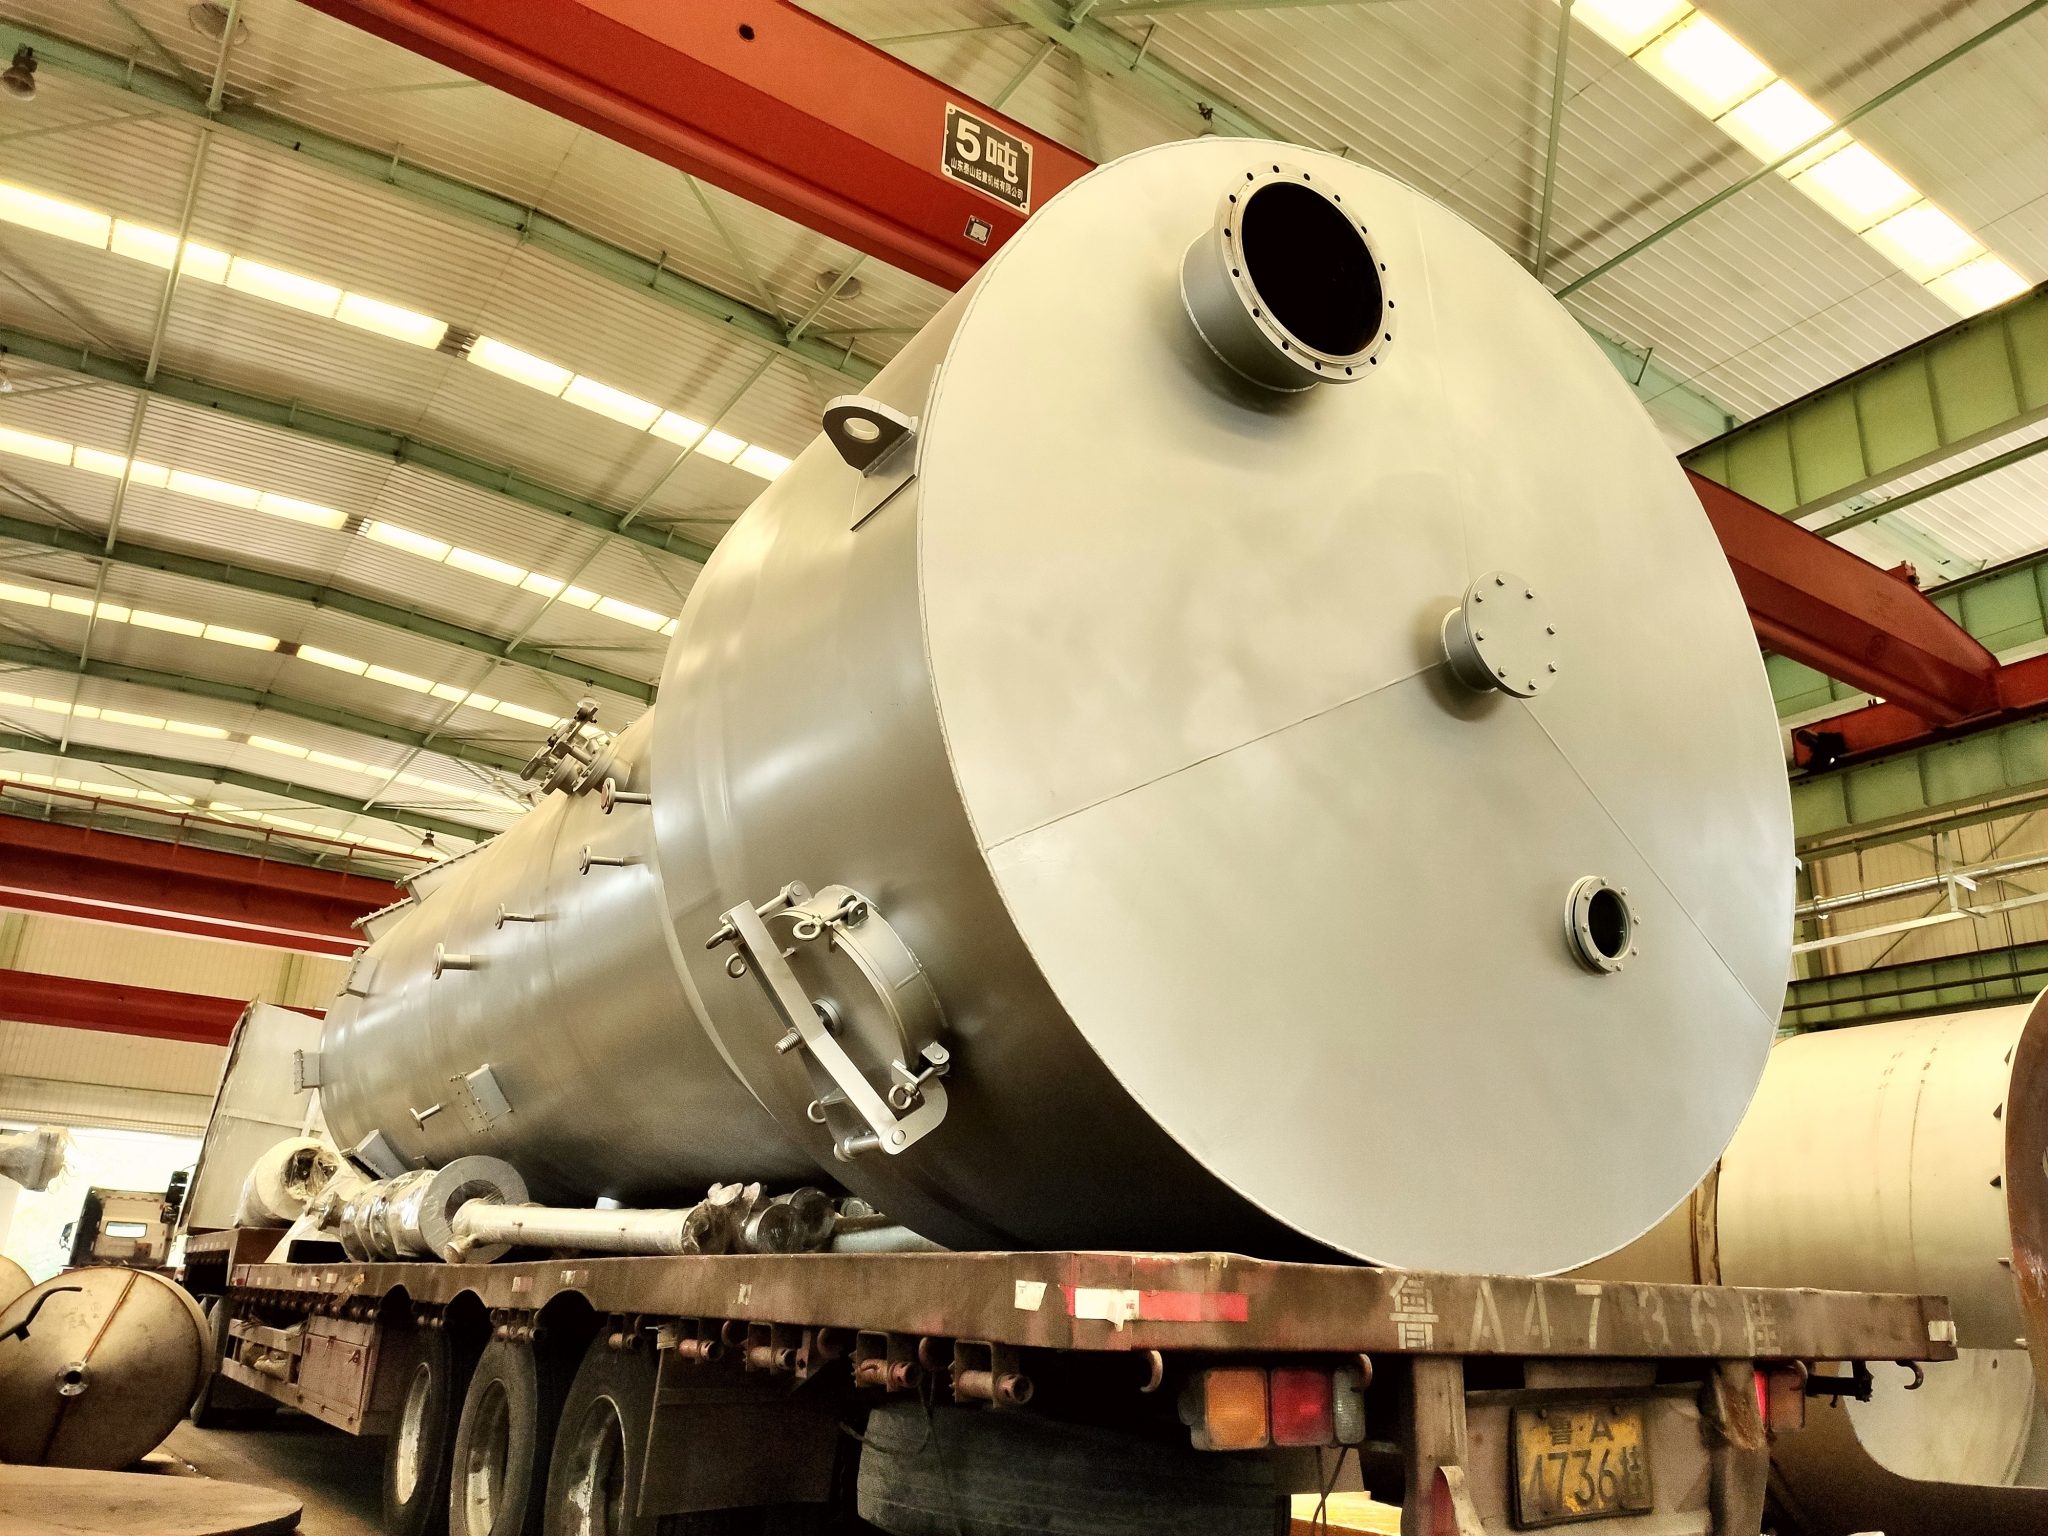
- Low-Temperature Desolventizing Stage: This is the decisive factor for product quality. CHEMSTA’s DTDC (Desolventizer Toaster Dryer Cooler) employs negative pressure low-temperature desolventizing technology, completing desolventizing, drying, and cooling in three stages at 60-80°C within 40-50 minutes total processing time.
- Quality Control Stage: Implementing real-time monitoring of protein solubility, solvent residue, and moisture content through automated inspection systems to ensure each batch meets food-grade standards.
Equipment Comparison – CHEMSTA DTDC vs Conventional Desolventizer
Conventional Desolventizer
Advantages:
- Lower equipment investment cost, 30-40% less than DTDC
- Simple operation with relatively less demanding operator skill requirements
Disadvantages:
- Desolventizing temperature of 100-110°C causes protein denaturation rates of 25-35%
- Solvent residue typically 800-1200 ppm, requiring additional treatment
- Product color is darker with L-value only 55-60, affecting downstream applications
- Higher energy consumption with steam usage of 1.2-1.5 tons/ton meal
CHEMSTA DTDC
Advantages:
- Low-temperature desolventizing (60-80°C) maintains protein solubility at 80-90%
- Solvent residue stable below 500 ppm, meeting international food-grade standards
- Excellent product color with L-value reaching 70-75, suitable for high-end protein products
- Optimized energy consumption with steam usage of only 0.8-1.0 tons/ton meal, saving 25-35%
Disadvantages:
- Higher equipment investment, 40-50% more than conventional equipment
- More demanding on process control precision, requiring skilled technical personnel
Data Comparison (According to CHEMSTA Internal Test Data 2024)
| Performance Metric | Conventional Desolventizer | CHEMSTA DTDC | Improvement |
|---|---|---|---|
| Desolventizing Temperature | 105-110°C | 60-80°C | -35-45% |
| Protein Solubility | 45-55% | 80-90% | +70-100% |
| Solvent Residue | 800-1200 ppm | <500 ppm | -50-60% |
| Steam Consumption | 1.2-1.5 tons/ton meal | 0.8-1.0 tons/ton meal | -25-35% |
| Annual Operating Cost (5000 tons/year) | $600,000 | $480,000 | -20% |
Conclusion: Although DTDC equipment investment is higher, the payback period is only 1.5-2 years, with significantly lower long-term operating costs and markedly improved product quality, making it ideal for factories targeting the food-grade protein product market.
Quality Standards – Meeting EU and US Market Requirements
Food-Grade Soybean White Flake Specifications
According to EU Regulation 2023/2005 and US FDA 21 CFR 184.1860 standards, food-grade soybean white flake must meet the following quality parameters:
| Quality Parameter | Food-Grade Standard | Feed-Grade Standard | Key Difference |
|---|---|---|---|
| Protein Content (dry basis) | ≥48% | ≥44% | +9% |
| Protein Solubility (NSI) | ≥75% | ≥45% | +67% |
| Solvent Residue | ≤500 ppm | ≤3000 ppm | -83% |
| Moisture | ≤12% | ≤13% | -8% |
| Urease Activity | 0.02-0.3 | ≤0.5 | Precise Control |
| Color (Hunter L-value) | ≥68 | – | Food-grade Only Requirement |
These standards represent not just regulatory requirements but quality thresholds that determine market access and product value. For producers targeting export markets to the EU and US, meeting these standards is essential for avoiding trade barriers and commanding premium pricing.
Industry Expert Perspective
“With the rapid growth of the plant-based protein market, demand for food-grade white flake has increased at15-20% annuallyover the past three years. However, there remains a shortage of high-quality white flake meeting international standards in the market, creating a tremendous market opportunity for producers adopting advanced low-temperature processes. According to our market research, producers capable of consistently manufacturing white flake meeting EU and US standards can maintain product premiums at25-35%over the long term.”— David Chen, Technical Director, American Soybean Association
This perspective reflects the industry’s urgent need for high-quality white flake. In fact, the Bunge Limited 2024 Protein Market Outlook report predicts that by 2028, global demand for food-grade white flake will reach 8.5 million tons, while current supply is only 6.2 million tons, representing a 2.3 million ton supply gap.
Implementation Guide – Investing in Soybean White Flake Production
Step-by-Step Investment Process
Step 1: Market Positioning and Target Market Selection
Action:
Define product target markets (food-grade SPC/SPI, feed-grade, export-oriented) and determine quality standard requirements. Food-grade products require meeting EU/US standards with higher investment costs but also higher returns.
Expected Results:
- Food-grade market: Product premium 25-35%, payback period 1.5-2 years
- Feed-grade market: Product premium 5-10%, payback period 2.5-3 years
- Export-oriented: Additional logistics costs 10-15%, but larger market capacity
Considerations:
Food-grade markets demand higher precision in equipment, process control, and quality traceability systems. Plan ahead for obtaining ISO 22000, HACCP, and other certifications before entering these markets.
Step 2: Equipment Selection and Process Design
Action:
Select appropriate equipment configurations based on capacity requirements. CHEMSTA provides complete production line solutions from 50 T/D to 3000 T/D, including core equipment:
- Drag Chain Extractor (Ring Extractor)
- DTDC Desolventizer Toaster Dryer Cooler (Integrated Desolventizing-Drying-Cooling Machine)
- Horizontal Filter
- Thin Film Evaporator
Expected Results:
- Equipment utilization: 85-92%
- Product qualification rate: ≥98%
- Energy consumption control: Steam usage 0.8-1.0 tons/ton meal
Considerations:
Equipment selection should comprehensively consider investment budget, capacity planning, and quality objectives. It is recommended to conduct a technical-economic analysis before determining the final solution.
Step 3: Project Implementation and Quality Control
Action:
Implement the project in phases, including civil engineering, equipment installation, commissioning, and personnel training. CHEMSTA provides EPC turnkey services, controlling project quality throughout from design to delivery.
Expected Results:
- Project timeline: 12-18 months
- Commissioning period: 2-3 months
- Personnel training: 1-2 months
Considerations:
Establish a comprehensive quality control system including four stages: raw material inspection, process monitoring, finished product testing, and data traceability.
Future Trends – The Growing Demand for High-Quality Soybean White Flake
Future Outlook
According to the Boston Consulting Group (BCG) 2024 Plant-Based Protein Revolution report, the food-grade white flake market will exhibit the following trends over the next five years:
- Demand Growth: By 2029, global food-grade white flake demand will reach 12 million tons, a 41% increase from 2024
- Quality Upgrade: 78% of downstream protein production enterprises require raw material protein solubility ≥85%, a 15 percentage point increase from 2024
- Technology Trend: Adoption rate of low-temperature desolventizing technology will increase from 45% in 2024 to 72% in 2029
- Market Premium: The price gap between high-quality white flake (protein solubility ≥85%) and regular products will expand to 40-50%
These trends indicate that the window of opportunity for upgrading production capacity is narrowing. Early adopters of advanced low-temperature technology will secure market advantages that latecomers will struggle to overcome.
Key Challenges
Challenge 1: High Equipment Investment Threshold
Severity: According to CHEMSTA 2024 Customer Survey, 62% of SMEs identify equipment investment as a major barrier
Response Strategy: Provide financing lease options, installment payment plans, reducing upfront investment pressure
Challenge 2: Shortage of Technical Personnel
Severity: 75% of enterprises report a lack of professional low-temperature process technical staff
Response Strategy: CHEMSTA provides technician training programs, remote technical support, establishing an expert consultation hotline
Challenge 3: Complex International Standards
Severity: Significant differences in food-grade protein product standards across countries, with 48% of export enterprises facing compliance challenges
Response Strategy: Provide standardized process packages, certification consulting services, assisting clients in obtaining EU, US, Halal, Kosher and other certifications
Conclusion
In summary, soybean white flake as a critical raw material in the plant-based protein value chain directly determines the market value and competitiveness of final protein products. According to the Grand View Research 2024 report, food-grade white flake produced using advanced low-temperature processes maintains a product premium of 25-35%, with market demand growing at 15-20% annually.
CHEMSTA, through DTDC low-temperature desolventizing technology, Drag Chain Extractor patented equipment, and other core offerings, provides complete production line solutions from 50 T/D to 3000 T/D for plant owners and project investors. Based on actual project data, production lines using CHEMSTA equipment achieve a payback period of only 1.5-2 years, with product quality stably meeting EU and US food-grade standards.
Facing the rapid growth of the global plant-based protein market, now is the strategic window for investing in production process upgrades and entering the high value-added food-grade market. As Bunge Limited CEO Greg Heckman stated at the 2024 Global Protein Summit: “Companies that invest in high-quality protein raw material production today will occupy the most advantageous position in the plant-based protein revolution of the coming decade.”
For plant owners and project investors considering entering or upgrading in this field, the message is clear: the technology is mature, the market demand is verified, and the economic returns are compelling. The question is not whether to invest, but when.
Core Equipment for Soybean White Flake Production
Success Stories
ABOUT CHEMSTA
CHEMSTA is a leading supplier of turnkey projects and equipment for plant oils & fats, soybean deep processing, and soybean protein, with nearly 50 years of experience.
We have built more than 1,000 plants worldwide, serving clients across 50+ countries. Our commitment to innovation, quality, and global expertise has earned us recognition as a trusted partner in industrial processing.
For more information about our soybean white flake production solutions, please contact us at [email protected] .