A Step-by-Step Guide to Setting Up a Peanut Oil Extraction Plant
Launching a high-performing Peanut Oil Extraction Plant is equal parts engineering, operations, and business discipline. This step-by-step guide distills what seasoned project owners, process engineers, and operators need to know—so you can move from feasibility to first oil with confidence. Drawing on CHEMSTA’s turnkey experience in oilseed pretreatment, extraction, and refining, we focus on practical decisions that determine yield, quality, uptime, and ROI.

Introduction
Peanut oil projects succeed when the design answers three questions early and concretely:
- What capacity and product grades will you supply?
- Which process route best balances yield, OPEX, CAPEX, and risk?
- How will the layout, utilities, and automation support safe, repeatable performance year-round?
1) Feasibility first: market, raw materials, and grade definition
Define the product slate up front. For a Peanut Oil Extraction Plant, typical slates include:
- Crude peanut oil (for onward refining)
- Refined, bleached, deodorized (RBD) peanut oil (salad/frying grades)
- By-products: peanut meal/cake (protein feed), lecithin (if recovered), spent bleaching earth management plan
Feasibility checklist
- Secured raw peanut supply (variety, seasonality, aflatoxin control programs)
- Target oil specs (FFA, color, odor, wax content, peroxide value) and packaging formats
- Offtake options for meal and by-products
- Utilities availability and cost (steam, power, cooling water, inert gas)
- Site logistics (inbound shells/unshelled peanuts, outbound bulk/pack)
CHEMSTA tip: treat aflatoxin risk as a design parameter, not just a QA step. It affects receiving, cleaning, storage, aeration, and meal handling protocols.
2) Capacity planning and line balancing
Right-sizing the Peanut Oil Extraction Plant means aligning:
- Daily throughput (t/day) with harvest peaks and storage constraints
- Unit operations so bottlenecks don’t migrate (cleaning → cracking → flaking → conditioning → pre-press → extractor → evaporation → DT/DC → refining)
- Maintenance windows (CIP, filter changeouts, scheduled inspections)
Decision anchors
- Pre-press/solvent line balance (press tonnage vs. extractor residence time)
- Refinery capacity vs. crude oil storage buffer
- Tank farm turnover (raw, crude, RBD) and truck/rail cadence
3) Raw peanut specifications and how they impact yield
Peanut condition at intake sets the upper bound on performance:
- Moisture and shell content drive flaking behavior, extractor percolation, and energy load.
- Foreign matter and stones threaten downstream equipment.
- Kernel integrity affects press cake structure and miscella quality.
- Aflatoxin control requires validated sampling plans, segregation, and documentation trails.
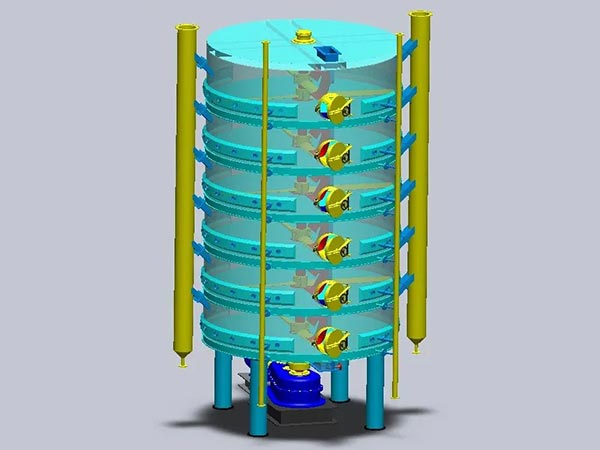
Design for robust receiving and preparation: scalpers, destoners, magnetic separation, dehulling/shelling, cracking, aspiration, conditioning, flaking. CHEMSTA integrates online monitoring (temperature, moisture) to stabilize preparation before extraction.
4) Pretreatment: getting press cake and flakes “just right”
Great extraction starts with great preparation. Objectives: uniform flake thickness, stable flake moisture, and consistent press cake porosity.
Top levers
- Conditioning to plasticize kernels for flaking without scorching proteins
- Flaker rolls set for repeatable thickness and minimal fines
- Pre-press to form a porous cake, reduce press oil load to the solvent system, and control residual oil in the meal
Operator focus points
- Keep fines under control to protect the extractor percolation and filtration steps.
- Maintain steady conditioner temperatures and residence time to avoid variable cake density.
5) Choosing the process route: pre-press + solvent vs. full-press
For peanuts, most industrial plants select pre-press + solvent extraction to hit low residual oil in meal and maximize overall yield. Smaller plants or specialty grades may choose full-press (mechanical only) for simplicity and solvent-free labeling.
Peanut Oil Extraction Plant – Process Options at a Glance
| Route | Typical scale | Yield potential | Oil quality profile | CAPEX/OPEX balance | When to choose |
|---|---|---|---|---|---|
| Full-press (mechanical) | Small to medium | Moderate; higher residual in cake | Lower phosphatide load; minimal solvent handling | Lower CAPEX; higher energy per ton | Niche volumes, solvent-free positioning, faster time-to-market |
| Pre-press + solvent | Medium to large | High, low residual in the meal | Consistent crude for efficient refining | Higher CAPEX; strong OPEX via high yield | In mainstream edible markets, the by-product meal value is critical |
CHEMSTA supplies both routes and can simulate yield/energy trade-offs against your raw peanut profile and product targets.
6) Extractor selection and solvent recovery strategy
Extractor geometry governs contact efficiency, percolation stability, and maintenance. Common choices include rotocell and loop/ring extractors with staged counter-current miscella flow.
Design essentials
- Residence time tuning (soak/drain cycles) for peanuts’ oil-rich matrix
- Robust fines management—screen decks, desanders, miscella polishing
- Solvent recovery via multi-effect evaporation and stripping, with condenser systems sized for peak flows
- Closed-loop solvent balance with leak detection and inventory reconciliation
Safety first: design for inerting, explosion protection, and ventilation in solvent areas. CHEMSTA’s solvent accounting toolkit supports compliance and loss reduction.
7) DT/DC (desolventizing-toasting/drying-cooling) and meal quality
The DT/DC bundle is where you stabilize meal protein and drive solvent to specification. Control points include:
- Tray temperatures and vapor contact to minimize over-toasting (protects protein value)
- Final meal moisture and temperature before storage or pelletizing
- Tail-gas handling to reduce VOCs and odors
Well-tuned DT/DC improves both food safety and economics: lower solvent losses, better meal value, and easier downstream handling.
8) Refining: degumming, neutralization, bleaching, deodorization (and winterization)
Peanut oil refining strategies depend on target grades:
- Water/acid/enzymatic degumming for phosphatide removal and lower losses
- Chemical neutralization for higher FFA crude, or physical refining when feasible, to minimize soaps and effluent
- Bleaching with optimized adsorbent blends and precise contact conditions
- Deodorization to polish flavor/odor and reduce residual FFA
- Winterization (dewaxing) for salad-grade clarity
CHEMSTA’s modular refineries scale from pilot to large continuous lines, with heat integration to reduce steam load and protect oil quality.
9) Utilities and site infrastructure you must get right
A reliable Peanut Oil Extraction Plant stands on its utilities. Undersized or unstable utilities become chronic bottlenecks and quality risks.
Utilities & Infrastructure – Planning Matrix
| System | What it serves | Key design notes | Risk if under-designed |
|---|---|---|---|
| Steam | Conditioner, DT/DC, evaporators, deodorizer | Header stability, condensate recovery, clean steam where required | Poor heat transfer, off-spec oil, energy waste |
| Cooling water/chilled loop | Condensers, deodorizer vacuum, winterization | Seasonal capacity, water quality, fouling control | Vacuum instability, low recovery, downtime |
| Power & UPS | Drives, controls, safety systems | Harmonics, redundancy for critical loops | Nuisance trips, unsafe states |
| Instrument air & nitrogen | Valve actuation, inerting, blanketing | Dryness spec, redundancy, monitored purity | Solvent safety compromise, oxidation risk |
| Effluent treatment | Neutralization, soaps, fines | Sizing for upset conditions, oil recovery | Compliance risk, off-odor, unplanned shutdowns |
| Tank farm | Crude, RBD, solvent | Layout, fire protection, inert gas, overfill prevention | Safety and quality incidents |
10) Quality assurance, food safety, and data you should capture from day one
Treat QA/QC as a design deliverable, not an afterthought. Build in sampling points, online analyzers where justified, and digital traceability.
Peanut Oil Extraction Plant – In-Process Quality KPIs
| Stage | KPI | Why it matters | Typical control action |
|---|---|---|---|
| Preparation | Flake thickness & moisture | Drives extractor percolation and yield | Adjust conditioner temp/residence; flaker gap |
| Pressing | Cake residual oil | Sets solvent duty and meal economics | Press load/shaft speed, choke settings |
| Extraction | Miscella concentration & fines | Affects evaporation load and fouling | Screen hygiene, fines removal, percolation tuning |
| Evap/Stripping | Solvent in crude oil | Refinery stability, safety | Heat balance, stripping steam, vacuum |
| Refining | FFA, phosphorus, color | Release criteria for RBD | Degumming route, caustic dose, bleaching earth |
| Deodorization | Odor, FFA tail, color stability | Consumer acceptance, shelf life | T-temp, vacuum, stripping rate, residence |
Document control plans, HACCP points, and rework rules. CHEMSTA’s automation integrates batch/lot genealogy and alarm analytics to support audits and continuous improvement.
11) Automation, safety, and commissioning


- Automation: Use layered control (PLC/DCS) with permissives and interlocks on solvent and hot-oil systems; add a historian for energy and yield KPIs.
- Process safety: Hazard identification, classified area design, gas detection, inerting logic, e-stop architecture, grounding/bonding, and ignition source control.
- Commissioning: Cold checks → loop checks → dry runs → heated circulation → solvent introduction → first oil → performance test. Define pass/fail gates and documentation before you start.
CHEMSTA’s commissioning playbooks accelerate ramp-up while protecting equipment and product quality.
12) By-products and sustainability: profit and compliance go together
- Meal: Maximize protein value by controlling DT/DC severity and particle size; consider pelletizing for logistics.
- Lecithin (if recovered): Degum route choice and drying conditions affect grade.
- Solvent and energy: Close solvent loss loops; apply heat integration (miscella/oil exchangers, MEE on evaporators).
- Waste: Manage spent bleaching earth to avoid self-heating; recover entrained oil where feasible. Design effluent neutralization and oil recovery with upset capacity in mind.
Table: Typical Functional Areas in a Peanut Oil Extraction Plant (and design priorities)
| Functional area | Core equipment | Primary objective | Design priority |
|---|---|---|---|
| Receiving & cleaning | Scalper, destoner, magnets | Remove FM and stones | High throughput, gentle handling |
| Preparation | Sheller, cracker, conditioner, flaker | Build an extractable structure | Tight moisture/temperature control |
| Pressing | Screw press/extruder | From porous cake, recover press oil | Stable cake density, low fines |
| Solvent extraction | Extractor, screens | Reduce residual oil in the cake | Percolation stability, solvent balance |
| Evaporation & recovery | Evaporators, strippers, condensers | Recover solvent, polish crude | Heat integration, fouling control |
| DT/DC & meal handling | DT/DC, cooler, pellet mill | Meal spec & solvent limit | Protein protection, safe storage |
| Refining | Degumming, neutralizing, bleaching, deodorizing, and winterization | Meet RBD spec | Controlled losses, flavor/clarity |
| Utilities & tank farm | Boilers, cooling, nitrogen, tanks | Plant stability & safety | Redundancy, protection, layout |
| Automation & QA | PLC/DCS, analyzers, lab | Control, traceability | Data integrity, alarm rationalization |
Conclusion
A successful Peanut Oil Extraction Plant is the product of disciplined decisions: a product-first design, preparation tuned to peanuts’ behavior, a matched extractor/solvent system, heat-tight solvent recovery, and a refinery calibrated to your grade targets. Build utilities and safety into the core, not the edges. Instrument what matters, and make QA visible in real time. That’s how you protect yield, quality, and uptime.
Ready to move from plan to plant?
CHEMSTA delivers pretreatment, pressing, extraction, and refining as integrated, turnkey solutions—backed by process guarantees, commissioning support, and operator training. Share your targeted capacity and product specs; we’ll return a tailored process route, mass/energy balance, and a phased CAPEX/OPEX model to guide your investment.
FAQ
What capacity is economical for a new Peanut Oil Extraction Plant?
Economics depend on raw material logistics and product slate. As a rule of thumb, align daily throughput with harvest peaks and tank farm turnover. CHEMSTA can model payback across multiple capacity cases.
Should I choose full-press or pre-press + solvent?
Full-press is simpler and solvent-free, but typically leaves more residual oil in the cake. Pre-press + solvent maximizes overall yield and is standard for large-scale edible markets. We simulate both with your peanut profile to quantify trade-offs.
How do I control aflatoxin risk in peanuts?
Design in sampling/segregation at intake, conditioned storage, and validated cleaning steps. Keep traceability end-to-end; protect meal value with controlled DT/DC severity.
What are the critical quality KPIs for refined peanut oil?
FFA, phosphorus, color, odor, and clarity post-winterization. Build release specs and in-process controls (degumming efficiency, bleaching earth dose, deodorizer vacuum/temperature).
How long does commissioning take?
Timeline depends on plant size and regulatory approvals. A staged plan—from cold checks to performance testing—reduces risk and accelerates stable production.
Can one site host peanut oil and vegetable protein projects together?
Yes, with layout and utilities planned for shared services and strict cross-contamination controls. CHEMSTA’s multi-line campuses reuse steam, cooling, and nitrogen to improve overall economics.