How Chemsta’s Turnkey Solutions Reduce Total Cost of Ownership
In the competitive global market for edible oils and fats, achieving an optimal Return on Investment (ROI) requires comprehensive control over project execution, operational costs, and product quality. This pursuit goes beyond simple volume processing; it demands minimizing project risk, reducing the Total Cost of Ownership (TCO), and maximizing the value extracted from every oilseed. Shandong Chemsta Machinery Manufacturing Co., Ltd. (CHEMSTA), a national high-tech enterprise operating since 1976, offers a proven method for optimizing ROI: integrated Turnkey Project Services.
CHEMSTA’s approach is centered on delivering an integrated solution that manages the entire project lifecycle—covering everything “From 0 to 100,” including all design, equipment manufacturing, installation, transportation, etc.. This integration is crucial for maximizing profitability in both Plant Oils & Fats and Vegetable Protein projects.
Table of Contents
The Turnkey Advantage: Reducing Project Risk and Total Cost of Ownership (TCO)
The typical process of building an industrial oil extraction plant involves coordinating multiple entities, often leading to cost overruns, compatibility problems, and significant delays. CHEMSTA’s integrated model, backed by nearly 50 years of expertise, mitigates these risks by centralizing control under one capable organization.
Integrated Solutions and Expertise
CHEMSTA operates as an entity integrating scientific research, production, operation, and service. This structure allows for seamless execution across all phases, from consultation to design and then to operation:
• Comprehensive Project Planning: We provide Overall Project Planning, Whole Plant Layout Design, Process Design, Equipment Manufacturing, Equipment Installation, Debugging, and after-service.
• Engineering Qualifications: The company holds qualifications in engineering design, pressure vessel (GB/ASME), and pressure pipeline design, manufacturing, and installation. Our commitment to quality is validated by achieving ISO9001 quality management system certification.
• Human Capital: Our strength is supported by a large technical team, including over 110 engineering and technical personnel, with over 50 senior engineers and 8 applied researchers.
Global Standards and Reliable Manufacturing
ROI relies heavily on the durability and safety of the equipment. CHEMSTA has demonstrated its manufacturing strength globally:
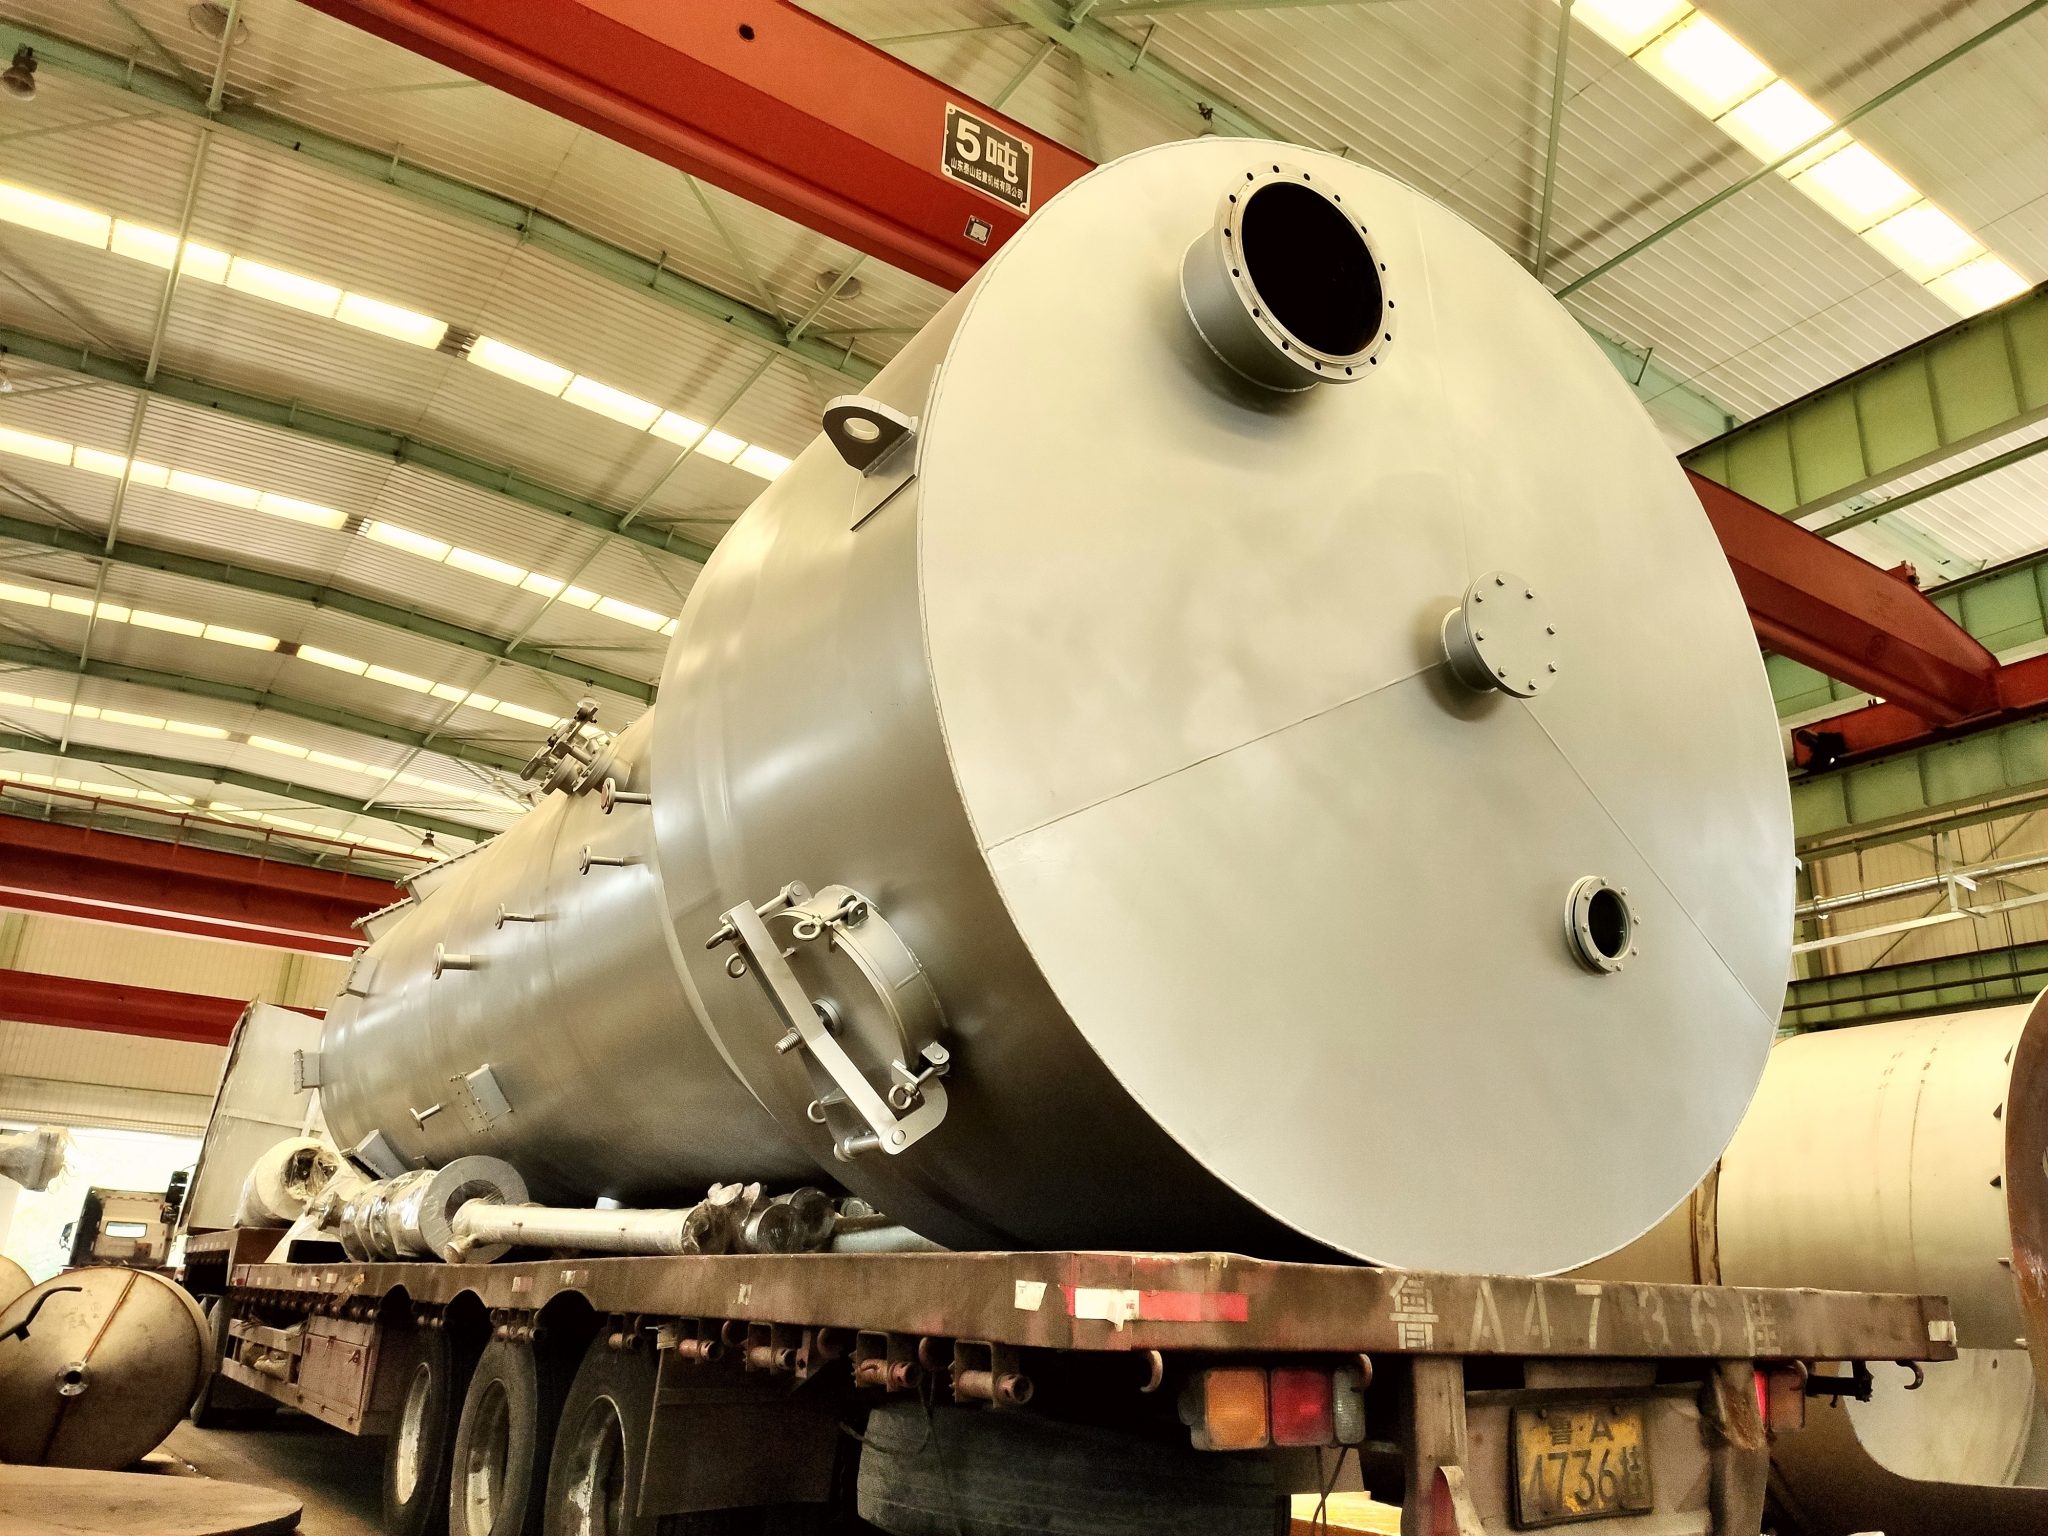
• ASME Certification: We have been a trusted global provider of high-quality ASME-standard pressure vessels since 2007. We have successfully delivered hundreds of ASME-compliant vessels to clients across the United States, Canada, the Philippines, and beyond.
• Industry Recognition: CHEMSTA is recognized as a National High-tech Enterprise, a National Contract-abiding Credit Enterprise, and a National SRDI “Little Giant” Enterprise.
Technological Drivers: Maximizing Operational Efficiency and Yield
The greatest impact on long-term ROI comes from minimizing energy and labor inputs while maximizing output yield. CHEMSTA’s dedication to innovation—investing more than 10% of annual sales revenue in R&D every year—ensures processes are highly efficient and intelligent.
Energy Saving and Scientific Recycling
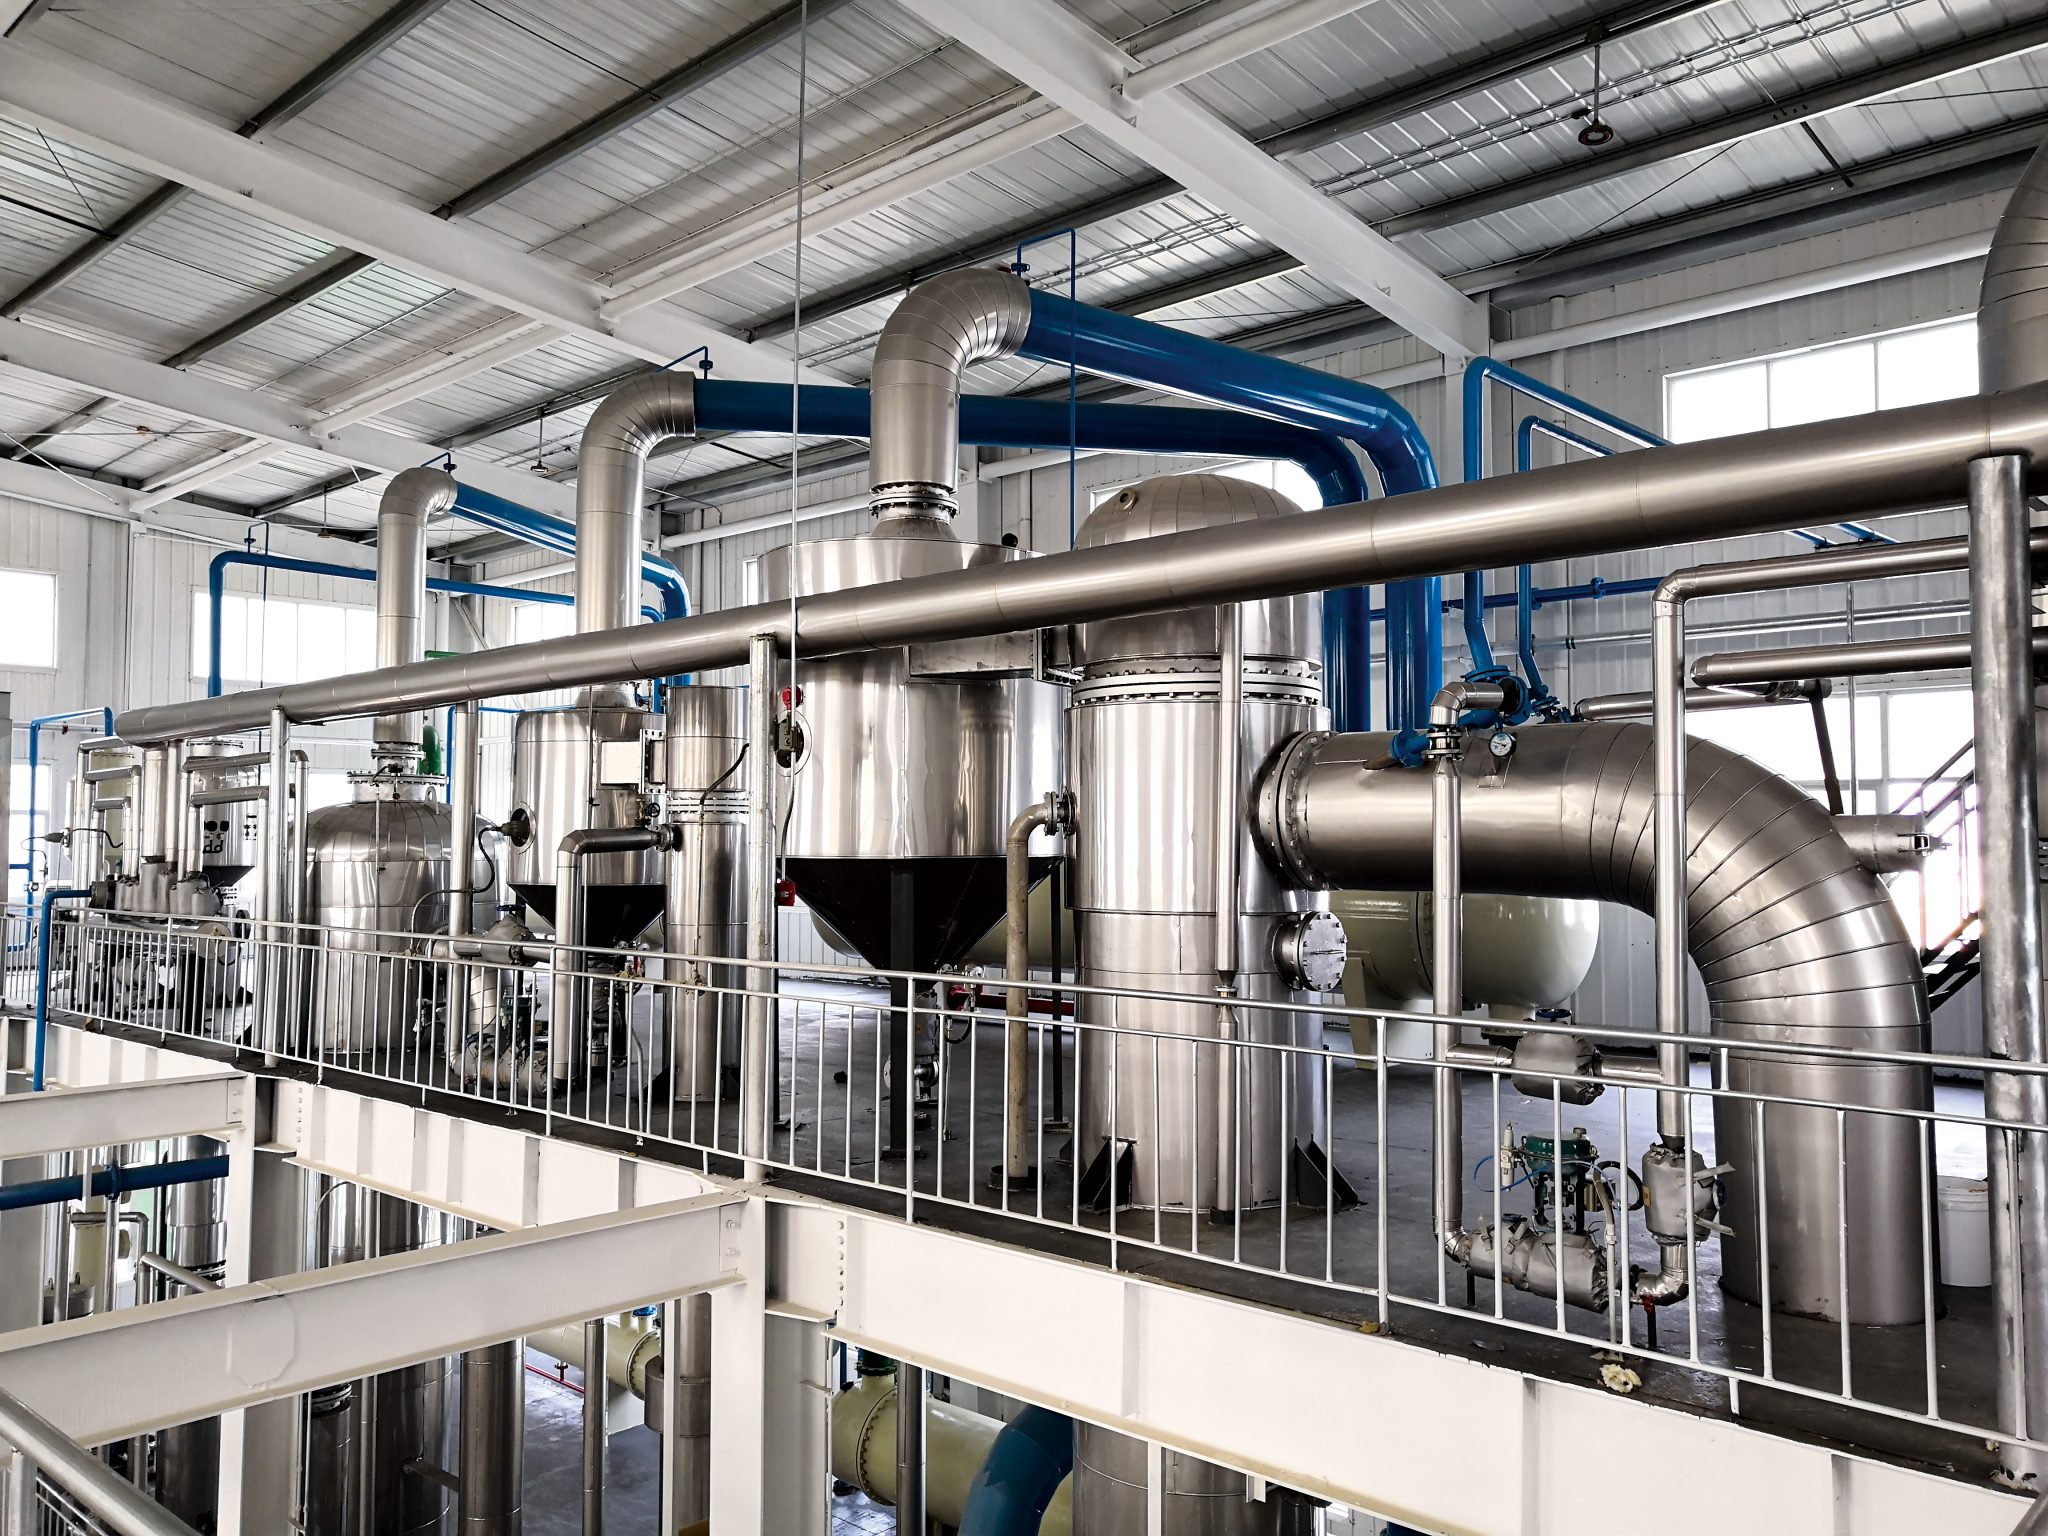
To achieve an operation that is “more energy-saving”, CHEMSTA utilizes international advanced energy-saving technology to optimize the process plan. Crucially, the heat of the system is scientifically and reasonably exchanged and recycled throughout the production process. This directly lowers utility costs, a major component of TCO.
Advanced Intelligence and Automation
Intelligent control guarantees stable operation and convenient production management. We use the most advanced automatic control technology in the world (such as SIEMENS PLC+WINCC) for automatic computer control of the entire production line.
Specialized High-Performance Equipment
CHEMSTA designs and manufactures specialized equipment that boosts efficiency. The D.T.D.C (Desolventizer Toaster Dryer Cooler) technology, for instance, is noted for improving vegetable oil and soy processing efficiency, improving oil yield and protein extraction, and reducing energy costs. Furthermore, our robust IP portfolio, including over 120 patent authorizations (17 invention patents) and 13 software copyrights, ensures clients receive technology that is mostly domestically leading, with some elements reaching the international leading level.
Enhancing Revenue Streams: From Oil to High-Value Byproducts
A successful ROI strategy leverages the production line to create high-value, high-margin products beyond standard crude oil. CHEMSTA’s solutions are designed to ensure the resulting product quality is more suitable for the deep processing of downstream products, thereby improving the yield and quality.
We provide equipment for processing a wide array of raw materials, including Soybean, Peanut, Sunflower, Corn Germ, Cotton Seed, Rapeseed, Rice Bran, and Palm Kernel. High-value processing capabilities include:
• Vegetable Protein: Complete set of equipment for Soybean Protein Concentrate (SPC) (alcohol method), Soybean Protein Isolate (SPI), Peanut Protein, and Cottonseed Protein. The technology development and industrialization of large-scale intelligent alcohol method production equipment for soybean protein concentration won the first prize of the Science and Technology Award of the China Grain and Oil Society.
• Refining and Lecithin: Solutions for Vegetable Oil Refinery Production Line and Phospholipid Concentrate and Fractionation Production Line. Projects include a 15t/d Soybean Phospholipid Concentrate Production Line in Vietnam and 3t/d Phospholipid Concentrate production lines.
• Natural Product Extraction: We also design and manufacture complete sets of equipment for the extraction and fractionation of natural products, such as Capsanthin Extraction and Marigold Extraction Production Line Projects.
FAQ
How does CHEMSTA reduce the TCO (Total Cost of Ownership) for extraction projects?
The TCO is significantly reduced through our comprehensive turnkey service model, which covers all aspects from design to installation and debugging. This centralized approach minimizes project risk, compatibility issues, and shortens the project cycle. Operationally, TCO is lowered by implementing international advanced energy-saving technology and ensuring the scientific recycling of system heat to reduce long-term utility costs. Furthermore, our equipment reliability is ensured by high standards, proven by our compliance with the America ASME Certificate.
What are CHEMSTA’s key technical advantages in increasing yield and reducing energy consumption?
Our technological edge is based on continuous innovation, with R&D investment exceeding 10% of annual sales revenue. We deploy the world’s most advanced automatic control technology, such as SIEMENS PLC+WINCC, to guarantee stable operation and facilitate efficient management. Key proprietary equipment, like the D.T.D.C., is designed specifically to boost vegetable oil and soy processing efficiency, improving oil yield and protein extraction, and reducing energy costs.
Does CHEMSTA manufacture equipment for high-value byproducts beyond standard edible oil?
Yes, maximizing revenue involves capturing high-value byproducts. CHEMSTA specializes in complete lines for high-margin products, including Phospholipid Concentrate and Fractionation, and deep processing of protein into Soybean Protein Concentrate (SPC) and Soybean Protein Isolate (SPI). We also supply lines for extracting natural pigments, such as Capsanthin Extraction and Marigold Extraction. The quality of the products produced is specifically designed to be highly suitable for downstream deep processing, enhancing their market value.
What is CHEMSTA’s experience in handling large-scale and complex international projects?
We have extensive experience in large-scale operations, having constructed hundreds of vegetable oil and protein plants in over 50 countries. Our portfolio includes benchmark projects such as the 3000 t/d Soybean Extraction Production Line Project and the 80,000 T/A SPC Production Line—the world’s largest single line. We also have a long-term partnership with Amur Agricultural Associated Enterprise in Russia, delivering both low-temperature meal and a 10,000 T/A SPI project.