Maximize ROI and Efficiency with a CHEMSTA Turnkey Edible Oil Processing Plant
Table of Contents
Introduction
Investing in an edible oil processing facility is a major undertaking. For investors and plant operators, the key concerns are maximizing return on investment (ROI), achieving high operational efficiency, and ensuring long-term reliability. CHEMSTA turnkey edible oil processing plants provide an integrated solution to these challenges. By combining engineering design, equipment supply, installation, commissioning, and operator training, CHEMSTA ensures that your plant is ready to deliver high-quality oil and protein by-products from day one. Unlike piecemeal setups, a CHEMSTA turnkey plant is designed as a cohesive system, reducing startup risks, avoiding hidden costs, and optimizing throughput.
This article explores every aspect of the plant, from raw material preparation to financial and operational optimization, providing a complete reference for investors and plant managers.
Why Choose a Turnkey Plant?
The term turnkey refers to a fully integrated solution where the supplier handles all aspects of design, engineering, procurement, and commissioning. For investors, this approach provides several advantages: faster time-to-market because the plant is ready for production immediately after commissioning, reduced operational risk due to pre-tested equipment and integrated automation, optimized workflow that reduces energy consumption, labor, and downtime, guaranteed quality from raw material handling to finished oil and protein, and long-term support through training, maintenance, and process optimization guidance. Turnkey plants provide not just equipment, but a complete operational ecosystem. For new investors or expanding producers, this reduces the complexity of managing multiple suppliers and ensures predictable results.
Raw Material Preparation: The Foundation of Efficiency
The quality and preparation of raw materials are crucial for maximizing oil yield and plant efficiency. Typical oilseeds include soybeans, sunflower, rapeseed, cottonseed, corn germ, and rice bran. Moisture content generally ranges from 8 to 12 percent depending on the raw material. Pre-treatment includes cleaning, dehulling if necessary, and flaking or pre-pressing. Uniform flake thickness and controlled moisture are essential. CHEMSTA plants employ low-temperature flaking to preserve protein integrity while enhancing oil extraction efficiency.
Recommended Raw Material Specifications
| Oilseed Type | Moisture Content (%) | Oil Content (%) | Flake Thickness (mm) |
|---|---|---|---|
| Soybean | 10–12 | 18–20 | 0.25–0.35 |
| Sunflower | 8–10 | 40–45 | 0.3–0.4 |
| Rapeseed | 8–10 | 38–42 | 0.3–0.35 |
| Cottonseed | 8–10 | 18–22 | 0.25–0.35 |
| Corn Germ | 9–11 | 40–45 | 0.25–0.35 |
| Rice Bran | 8–10 | 15–20 | 0.2–0.3 |
High-quality raw materials ensure higher oil yield, better protein retention, and reduced process variability, which directly translates into higher ROI.
Full Process Flow: From Raw Material to Refined Oil
CHEMSTA turnkey plants integrate every stage of the oil processing workflow.
Cleaning and Dehulling
Cleaning and dehulling remove stones, dust, metal fragments, and hulls, preventing equipment damage, improving extraction efficiency, and ensuring finished oil quality.
Flaking and Pre-Pressing
Low-temperature flaking and pre-pressing remove part of the oil mechanically while preserving protein structure.
Solvent Extraction (Optional)
Solvent extraction maximizes oil recovery from flakes or cake, with optimized solvent-to-material ratios and extraction times achieving recovery rates above 97 percent.
Refining
Refining steps include degumming, neutralization, bleaching, deodorization, and optional winterization or fractionation, with automated controls ensuring consistent free fatty acid levels, oil color, and stability.
By-product Handling
Defatted meal and protein concentrates are processed as by-products for feed or food applications, creating additional revenue streams.
Typical Efficiency Parameters
| Process Stage | Key Metric | Target |
|---|---|---|
| Flaking | Moisture | 8–10% |
| Pre-Press | Oil Removal | 50–60% |
| Solvent Extraction | Oil Recovery | 97%+ |
| Refining | FFA | <0.1% |
| Bleaching | Color | <10 Lovibond |
| Deodorization | Peroxide Value | <1 meq/kg |
Operational Efficiency: Automation and Control
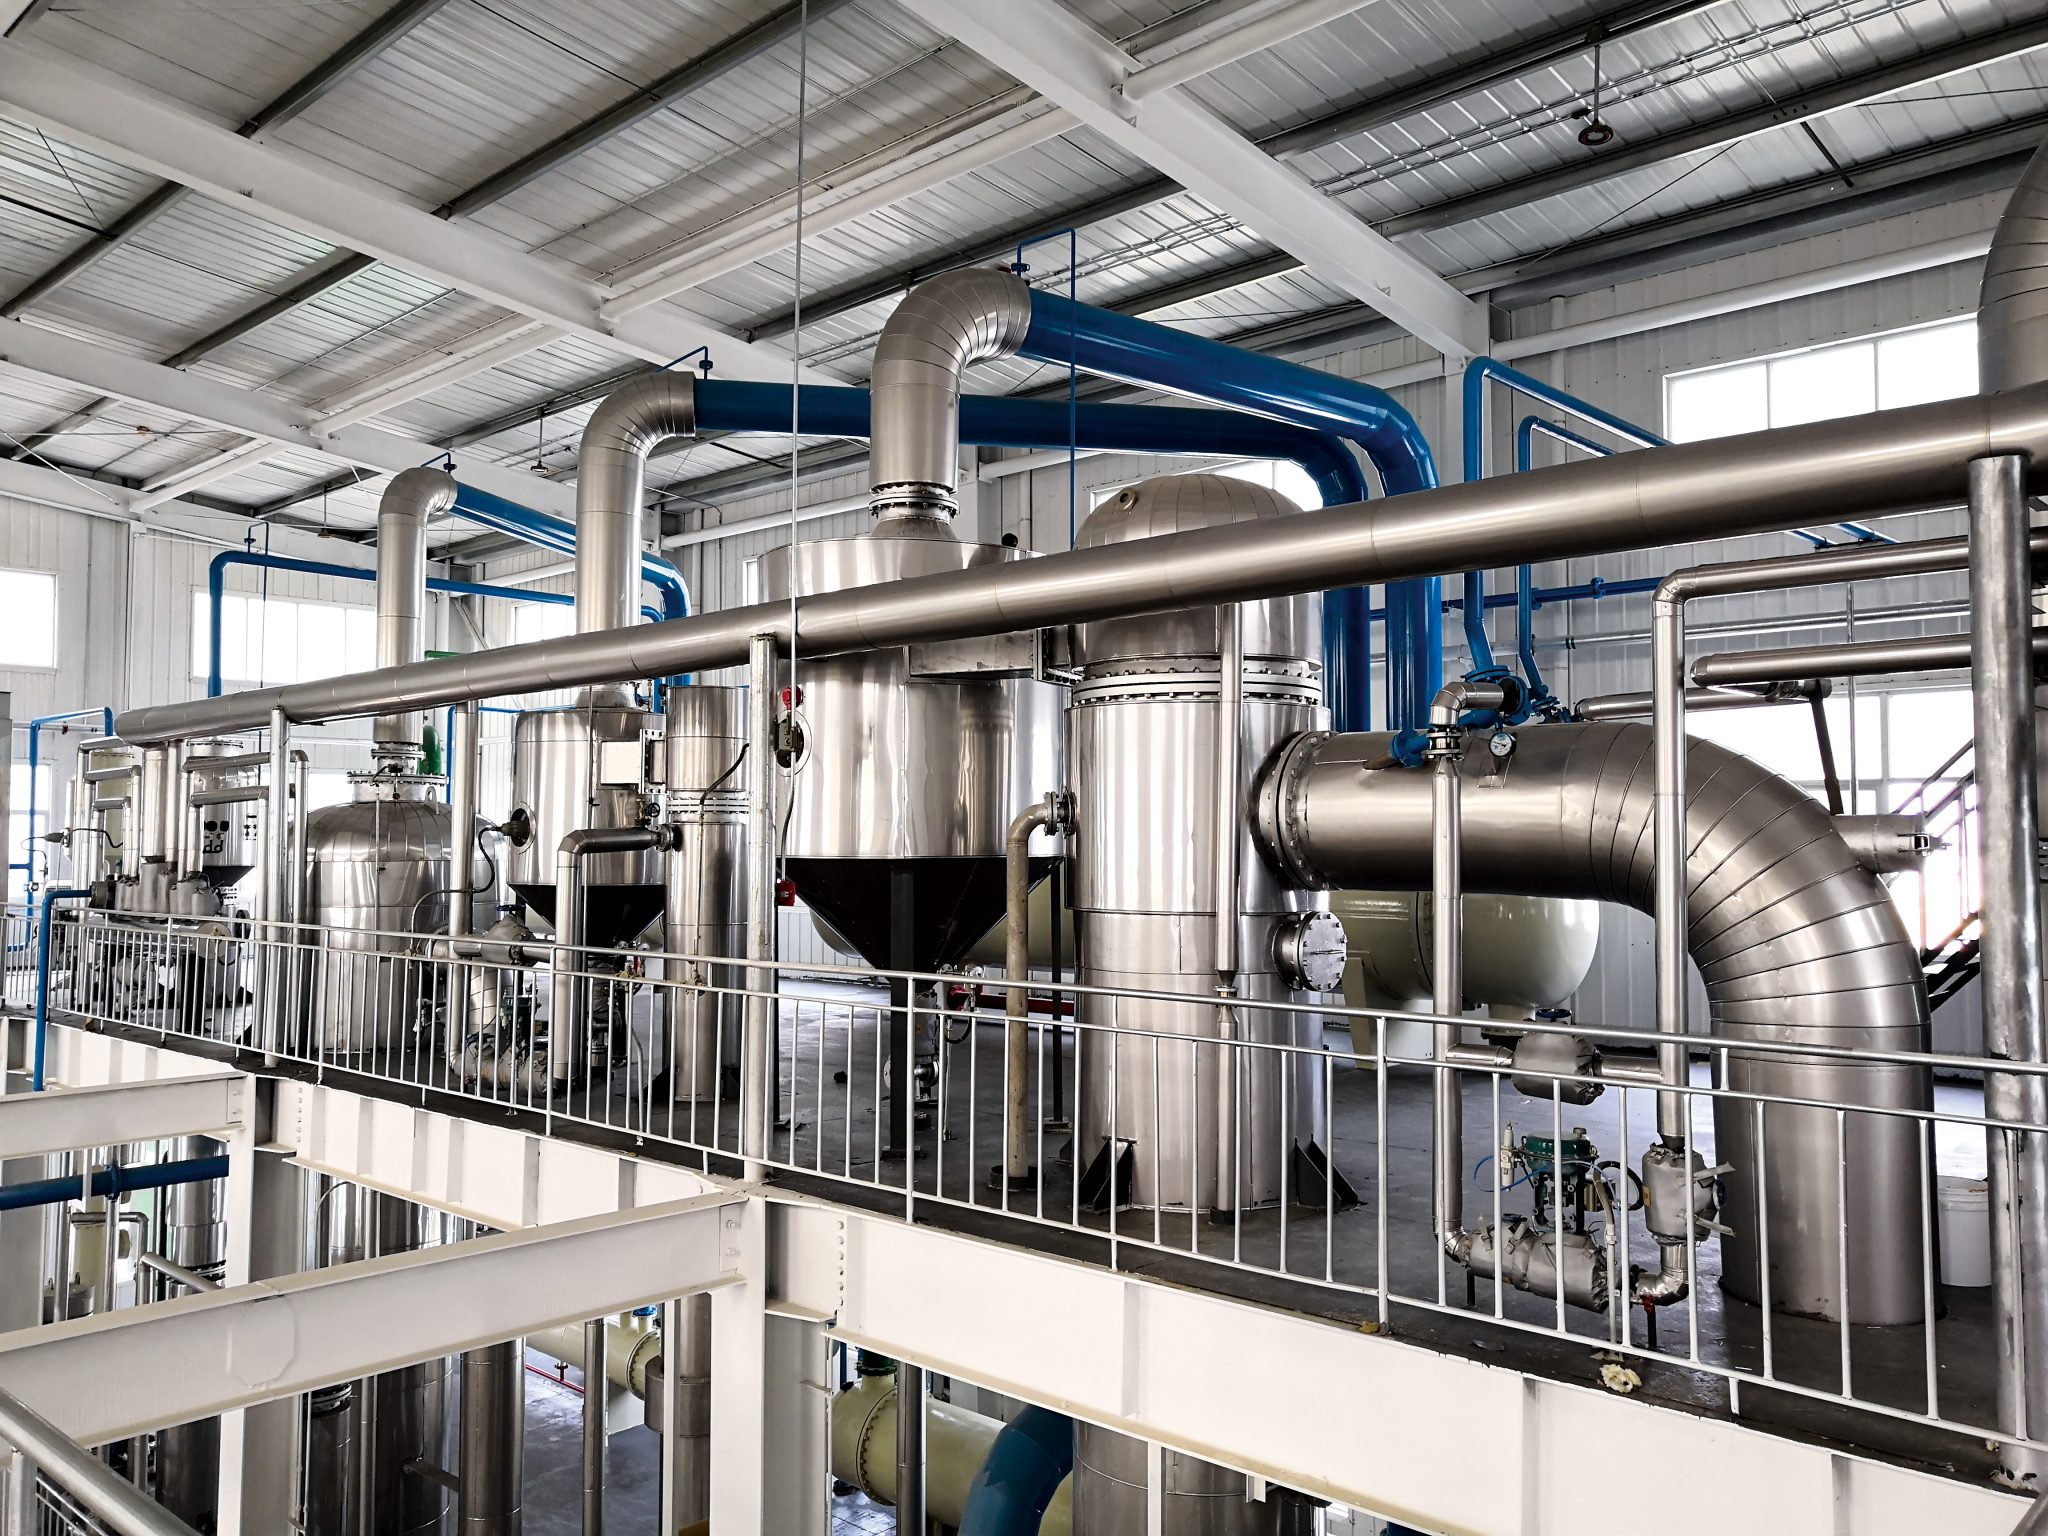
CHEMSTA turnkey plants utilize centralized automation systems to manage temperature, vacuum, and pressure in refining and extraction, flow rates and oil levels in tanks, real-time alarms for deviations, and data logging for process optimization and regulatory compliance. Automation reduces labor costs, prevents human errors, and ensures repeatable product quality.
Energy Optimization and Cost Control
Energy efficiency is a key factor in ROI. CHEMSTA plants integrate heat recovery from deodorization and refining stages, vacuum-assisted processes to reduce steam consumption, efficient solvent recovery, and continuous monitoring to detect inefficiencies.
Energy Consumption Comparison
| Stage | Standard kWh/ton | CHEMSTA Optimized kWh/ton | Savings (%) |
|---|---|---|---|
| Degumming | 50 | 42 | 16 |
| Neutralization | 40 | 35 | 12 |
| Bleaching | 60 | 50 | 17 |
| Deodorization | 120 | 105 | 13 |
| Total | 270 | 232 | 14 |
Energy savings reduce operating costs and accelerate ROI.

Investment and ROI Analysis
CHEMSTA turnkey plants are designed for predictable and measurable returns.
| Plant Type | Capacity (tons/day) | Initial Investment ($) | Oil Yield (%) | Estimated ROI (Years) |
|---|---|---|---|---|
| Small | 10–20 | 1,000,000 | 90 | 4.5 |
| Medium | 50–200 | 3,500,000 | 95 | 3.0 |
| Large | 500+ | 10,000,000 | 97 | 2.8 |
Although turnkey plants may have a higher upfront cost, improved efficiency, higher oil yield, and energy savings reduce the payback period significantly.
Safety, Compliance, and Environmental Responsibility
Operational risks such as downtime, equipment failure, and inconsistent product quality are mitigated through factory-tested equipment, comprehensive documentation including SOPs and maintenance manuals, on-site commissioning and operator training, remote monitoring options, and safety measures including explosion-proof designs, dust collection, and solvent containment systems. CHEMSTA turnkey plants meet international safety and environmental standards, ensuring long-term regulatory compliance.
Maximizing Long-Term Profitability
Long-term profitability depends on consistent product quality, energy optimization, by-product utilization, and scalability. Stable oil color, low free fatty acids, and high shelf-life increase market competitiveness. Defatted meals can be sold as animal feed or processed into protein concentrates. CHEMSTA turnkey plants are modular, allowing investors to expand production capacity as demand grows.
Case Study: 50-Ton/Day CHEMSTA Turnkey Plant
Oil yield increased from 90 percent to 97 percent, energy savings were 12 percent compared to a previous piecemeal setup, ROI period decreased from 4.5 years to 2.8 years, and the plant was smoothly integrated with downstream refining and protein processing lines. This highlights the financial and operational benefits of choosing a CHEMSTA turnkey solution.
FAQ
Why choose a turnkey plant over individual equipment purchases?
Turnkey plants reduce project risk, accelerate commissioning, and maximize oil recovery and ROI.
Can CHEMSTA plants process multiple oilseed types?
Yes, they handle soybean, sunflower, rapeseed, cottonseed, corn germ, and rice bran.
How does automation improve efficiency?
Automation ensures precise control over process parameters, reduces labor costs, and maintains consistent product quality.
What is the typical payback period for a CHEMSTA turnkey plant?
Most plants achieve ROI within 2.5–3.5 years depending on raw materials and plant capacity.
Are CHEMSTA turnkey plants safe and environmentally compliant?
Yes, all turnkey plants comply with HACCP, ISO 22000, and local regulations.
Need Help Maximizing ROI with a CHEMSTA Turnkey Edible Oil Processing Plant?
If you’re unsure which CHEMSTA turnkey plant best fits your raw materials or production goals, our experts are here to help. Contact us today for a personalized consultation and get a complete turnkey solution designed for efficiency, reliability, and high-quality oil production. Don’t wait—get in touch now to start optimizing your oil processing operation with CHEMSTA.